
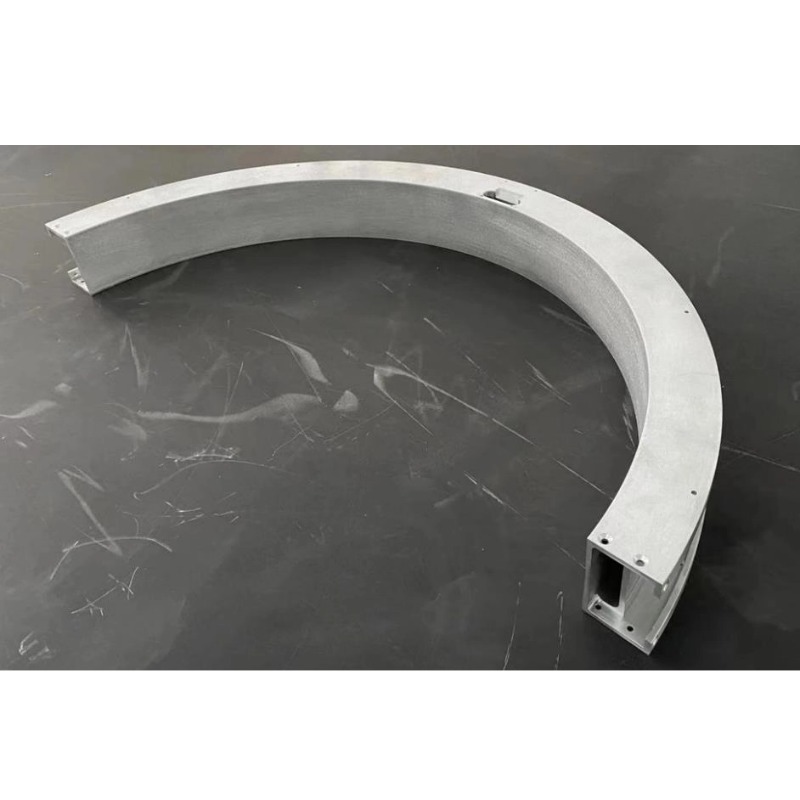
Custom Aluminum Profiles
Aluminum profile bending integrated mold opening
Integrated mold opening and customization for aluminum profile bending deeply integrates mold opening and customization
Product Details
Integrated mold opening and customization for aluminum profile bending deeply integrates mold opening and customization with precision bending, providing a one-stop service for the entire process from exclusive cross-section design, mold development, profile extrusion (cooperative production line) to CNC bending, CNC precision machining, and surface treatment. Under the traditional segmented procurement model, mold opening and bending belong to different manufacturers. Mold designers do not understand the bending process, bending masters do not understand the mold structure, and cross-sectional design is disconnected from the bending process. At best, repeated trial and error wastes time, and at worst, the profiles are scrapped and cannot be delivered. In the integrated mode, the mold design and bending process are coordinated by the same technical team, considering bending feasibility from the section design stage, and simultaneously planning the bending sequence and tolerance allocation.
01 Quality starts with raw materials
It is produced using A00 virgin aluminum ingots, containing no waste aluminum, with pure materials and stable mechanical properties. Depending on the bending conditions, materials such as 6063-T5 (low rebound, suitable for bending) and 6061-T6 (high strength, heavy load structure) can be selected to ensure bending quality from the source.
02 Collaborative optimization of mold design and bending process
Mold opening involves simultaneously planning the bending sequence and tolerance allocation. Issues such as the cumulative error of multi-segment bending, the cracking risk of thin-walled bending, and the rebound compensation of thick-walled bending are addressed in the mold design stage to ensure that the profile is in place in one go from mold opening to bending. Each section is independently designed with its own mold and does not share existing molds.
03 Precision bending and precision control
Equipped with precision equipment such as CNC bending machines, it can complete various bending forms such as L-shaped bending, U-shaped groove, Z-shaped border, right-angle bending, obtuse-angle bending, acute-angle bending, and special-shaped bending. The bending angle tolerance is ±1°, and the cumulative bending deviation of multiple segments is ≤±2mm. The maximum bending length is 6500mm, and the wall thickness ranges from 0.8mm to 6mm.
04 High-precision CNC machining
Equipped with precision equipment such as a five-axis CNC machining center, it can complete deep machining processes such as precision cutting of bent profiles, end face milling, drilling and tapping of mounting holes. The machining accuracy is ±0.01-0.005mm, and the stroke of multiple imported machine tools and ultra-long aluminum profile machining centers can reach 6.5 meters.
05 One-stop delivery of the entire process
From extrusion and bending to CNC finishing and surface treatment, one-stop delivery allows customers to connect with only one supplier, effectively solving the quality dispute caused by "separate mold opening and bending to find manufacturers". Dimension inspection report and material inspection report are provided for each batch.
Processing capacity parameters:
| Project | Parameters / Description |
|---|---|
| Applicable scenarios | Equipment frame bending, special-shaped structural parts, multi-section bending profiles |
| Optional materials | 6063-T5 (low rebound), 6061-T6 (high strength) |
| maximum circumscribed circle | 600-700mm |
| dimensional tolerance | ±0.02mm to ±0.04mm |
| bending form | L-shaped, U-shaped, Z-shaped, right angle, obtuse angle, acute angle, special-shaped bending |
| Bending angle tolerance | ±1° |
| Multi-segment bending cumulative deviation | ≤±2mm |
| bending wall thickness range | 0.8mm-6mm |
| Maximum bending length | 6500mm |
| CNC machining accuracy | ±0.01-0.005mm |
| surface treatment | Anodic oxidation, hard oxidation, electrostatic spraying |
| Execution Standards | GB/T 6892-2023 High-precision |
| mold opening cycle | Sampling for conventional structures takes 10-15 days. |
| minimum order quantity | Supports 50kg R&D prototyping |
| Production origin | Shanghai Qingpu |
Integrated mold opening and bending vs. segmented procurement:
| Comparison term | Segmented procurement | integrated mold opening and bending |
|---|---|---|
| Die design and bending process | Disconnected, each acting independently | Collaborative optimization, all in one go |
| Quality Responsibility | Mutual buck-passing | Unified responsibility |
| delivery control | Each link is independent and uncontrollable. | Unified production scheduling and controllability |
| cumulative error | Superimposition of each link | control within the same system |
Typical application scenarios:
special-shaped frame bending structure of automation equipment
non-standard equipment frame integrated forming
robot workstation bending profile
curved guide rail frame of intelligent logistics equipment
multi-bending structural components of industrial cabinet
detection equipment special-shaped frame
special angle bending structural member
multi-section continuous bending equipment frame
new energy equipment bending structural components
FAQ (Frequently Asked Questions)
Q1: What are the differences between integrated mold opening and customization of aluminum profile bending and ordinary segmented procurement?
A: Under the traditional segmented procurement model, mold opening and bending belong to different manufacturers. Mold designers do not understand the bending process, bending masters do not understand the mold structure, and cross-sectional design is disconnected from the bending process. At best, repeated trial and error wastes time, and at worst, the profiles are scrapped and cannot be delivered. In the integrated mode, the mold design and bending process are coordinated by the same technical team. The feasibility of bending is considered from the section design stage, and the bending sequence and tolerance allocation are planned simultaneously to ensure that the profile is in place in one go from mold opening to bending. Quality responsibility is unified and there is no passing the buck.
Q2: How to solve the problems of bending cracking and springback in customized integrated mold opening for aluminum profiles?
A: Mold opening involves simultaneously planning the bending sequence and tolerance allocation. Issues such as the cumulative error of multi-segment bending, the cracking risk of thin-walled bending, and the spring back compensation of thick-walled bending are addressed in the mold design stage. For thin-walled bending (0.8mm-2mm), 6063-T5 material (good elongation and low rebound) is used, and the bending radius is controlled at ≥2-3 times the wall thickness; Thick-walled bending (4mm-6mm) is equipped with a large-tonnage CNC bending machine and an accurate spring-back compensation algorithm, with a bending angle tolerance of ±1°. From the source, the profile is guaranteed to be in place in one go from mold opening to bending.
Q3: What bending forms are supported by integrated mold opening customization for aluminum profile bending?
A: Supports various bending forms such as L-shaped bending, U-shaped groove, Z-shaped border, right-angle bending, obtuse-angle bending, acute-angle bending, and irregular-shaped bending. The maximum bending length is 6500mm, and the wall thickness ranges from 0.8mm to 6mm. The cumulative deviation of multi-segment bending is ≤±2mm, meeting the high-precision assembly requirements of non-standard equipment frames and complex bending structural parts.
Q4: What is the accuracy of integrated mold opening and customization for aluminum profile bending?
A: Dimensional tolerance ±0.02mm to ±0.04mm, bending angle tolerance ±1°, cumulative deviation of multi-segment bending ≤±2mm. It is equipped with a five-axis CNC machining center to complete deep machining processes such as precision cutting of bended profiles, end face milling, drilling and tapping of mounting holes, with a machining accuracy of ±0.01-0.005mm, and can produce ultra-large materials with a circumscribed circle diameter of 600-700mm.
Q5: What materials can be used for customized integrated mold opening and bending of aluminum profiles?
A: Depending on the bending conditions, 6063-T5 (low rebound, good elongation, suitable for most bending scenarios, thin-walled bending is preferred) and 6061-T6 (high-strength, heavy-load structure, thick-walled bending is preferred) can be selected. Produced using A00 virgin aluminum ingots, containing no waste aluminum, the material is pure and has stable mechanical properties, ensuring bending quality from the source.
Q6: What is the minimum order quantity and delivery time for integrated mold opening and customization of aluminum profile bending?
A: The minimum order quantity supports 50kg-level R&D sampling. The conventional structural mold opening cycle is 10-15 days for sampling, and the batch delivery date is 12-18 days after the sample is confirmed. Because integrated bending mold opening involves the coordination of extrusion and bending processes and the adjustment of bending parameters, the delivery time is longer than that of pure mold opening customization. It is recommended to communicate the bending form and structural design in advance.
GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:Aluminum profile bending integrated mold opening