
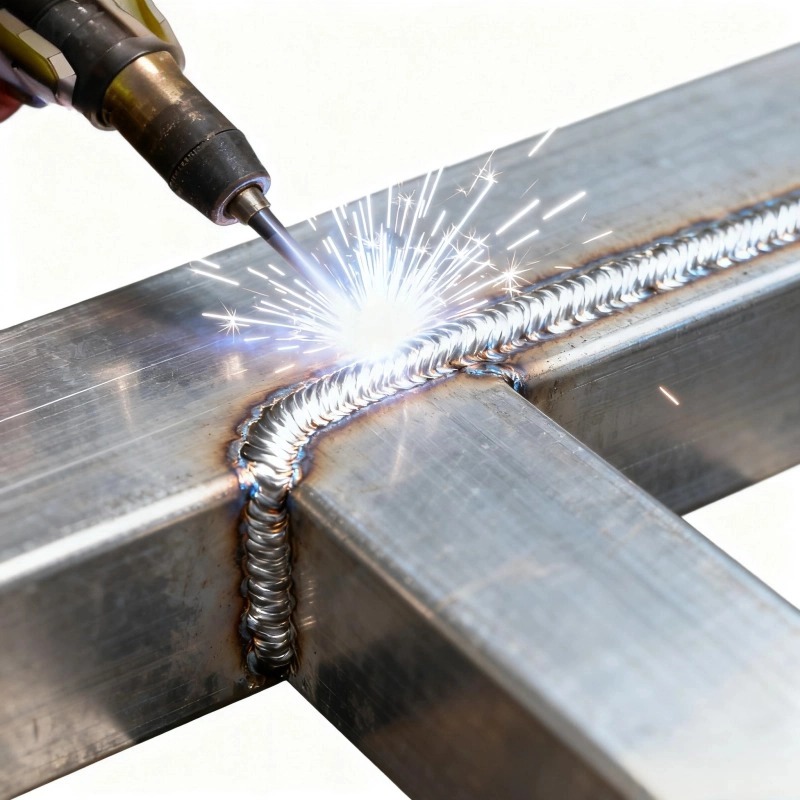
Custom Aluminum Profiles
Aluminum profile welding integrated mold opening
Integrated mold opening and customization for aluminum profile welding deeply integrates mold opening and customization
Product Details
Integrated mold opening and customization for aluminum profile welding deeply integrates mold opening and customization with precision welding, providing a one-stop service for the entire process from exclusive cross-section design, mold development, profile extrusion (cooperative production line) to CNC precision machining, precision welding assembly, and surface treatment. Under the traditional segmented procurement model, mold opening, extrusion, and welding belong to different manufacturers. Profile factories only care about extrusion and not the welding process, and welding factories only discover that the cross-section is unsuitable for welding or the design is unreasonable when they receive the profiles. In the integrated mode, welding engineers and extrusion engineers work together, considering welding feasibility from the section design stage to ensure that the profiles are in place from mold opening to welding assembly in one go.
01 Quality starts with raw materials
It is produced using A00 virgin aluminum ingots, containing no waste aluminum, with pure materials and stable welding performance. Various materials such as 6061-T6 (high-strength welded structure), 6063-T5 (general-purpose welded frame), 6005-T6 (fatigue-resistant welded structure), and 5083 (corrosion-resistant welded structure) can be selected according to the stress conditions and welding requirements of the welded structure. Aluminum alloy frame structures have the advantages of high specific strength, light weight, good corrosion resistance, easy processing and installation, and recyclability. The welding structure design can effectively improve the connection strength and achieve high-strength structural support compared to the standard aluminum profile assembly parts connection method.
02 Welding-friendly cross-section design
Mold opening involves simultaneously planning key elements such as weld bead position, weld bevel, welding space, deformation compensation, and weight reduction hole arrangement. The weld layout and structural rigidity of multi-piece splicing are optimized simultaneously to ensure that the profile is in place from mold opening to welding assembly in one go, avoiding the passive situation of "the profile is opened but the welding process cannot keep up". Each section is independently designed with its own mold.
03 Large-tonnage extrusion and high-precision control
Relying on the cooperative production line with an extrusion capacity of 600T to 12000T, it can produce ultra-large materials with a circumscribed circle diameter of 600-700mm. The closed-loop extrusion process controls the temperature and extrusion speed, and is accompanied by an artificial aging process to release internal stress, ensuring that the straightness and flatness of the frame profile are controllable. Dimensional tolerances are stably controlled within ±0.02mm to ±0.04mm.
04 Multi-process precision welding capabilities
Aluminum alloy welding is the core link in the deep processing of aluminum profiles, and its welding quality is greatly affected by the material properties. It is necessary to solve problems such as oxide film removal, pore control, hot crack prevention, and welding deformation control. Equipped with professional welding and assembly capabilities, and equipped with various welding processes such as MIG/TIG argon arc welding, gas shielded welding, and friction stir welding. It can complete precision welding and modular assembly of aluminum profile frames, with weld strength ≥ 85% of the base material. Products welded using friction stir welding technology have high weld strength, small deformation, and no pores, making them suitable for scenarios with high requirements for welding quality. The dimensional accuracy of the frame after welding can be controlled within ±1mm/3m.
05 One-stop delivery service
From extrusion and CNC finishing to welding, assembly, and surface treatment, the entire process is delivered in one stop, and customers only need to connect with one supplier. Welding quality inspection reports are provided for each batch, and key welds are traceable. It is suitable for various welding structural component scenarios such as large equipment frames, racks, conveyor line supports, and testing equipment frames.
Processing capacity parameters:
| Project | Parameters / Description |
|---|---|
| Applicable scenarios | Large equipment frames, racks, conveyor line supports, welded structural parts |
| Optional materials | 6061-T6, 6063-T5, 6005-T6, 5083 |
| Execution Standards | GB/T 6892-2023 High precision, compatible with EN 15085-2 |
| welding process | MIG/TIG argon arc welding, gas shielded welding, friction stir welding |
| weld strength | ≥85% of base material |
| Dimensional accuracy after welding | ±1mm/3m |
| maximum circumscribed circle | 600-700mm |
| dimensional tolerance | ±0.02mm to ±0.04mm |
| CNC machining accuracy | ±0.01-0.005mm |
| Maximum machining length | 6500mm |
| surface treatment | Anodizing, hard oxidation, powder spraying |
| matching processing | CNC finishing, welding and assembly |
| extrusion equipment | 600T-12000T (cooperative production line) |
| mold opening cycle | Sampling for conventional structures takes 10-15 days. |
| Batch delivery time | 15-20 days after sample confirmation |
| minimum order quantity | Supports small batch customization |
| Production origin | Shanghai Qingpu |
Comparison of integrated open-mold welding vs. segmented procurement:
| Comparison term | Segmented procurement | integrated mold opening welding |
|---|---|---|
| Section Design and Welding Process | disconnect | collaborative optimization |
| welding deformation control | If the extrusion plant is ignored, the welding plant will be difficult to control. | Mold opening stage is planning deformation compensation |
| Quality Responsibility | Mutual excuses | Unified responsibility |
| weld design | welding plant passive adaptation | Synchronous optimization during mold opening |
Typical application scenarios:
large-scale equipment frame welding assembly
Automated production line frame welding and assembly
conveyor line bracket welding structure
robot workstation welding frame
inspection equipment welding frame
welding frame of new energy equipment
special vehicle body welding structure
energy storage equipment welding frame
FAQ (Frequently Asked Questions)
Q1: What are the differences between integrated mold opening and customization for aluminum profile welding and segmented procurement?
A: Under the traditional segmented procurement model, mold opening, extrusion, and welding belong to different manufacturers. Profile factories only care about extrusion and not the welding process, and welding factories only find that the cross-section is not suitable for welding or the design is unreasonable when they receive the profiles. In the integrated mode, welding engineers and extrusion engineers work together, considering welding feasibility from the section design stage—key elements such as weld bead location, weld bevel, welding space, deformation compensation, and weight-reducing hole arrangement are planned simultaneously. Ensure that the profiles are in place from mold opening to welding assembly in one go, avoiding the passive situation where "the profiles are opened but the welding process cannot keep up". Quality responsibility is unified and there is no shirking of responsibility.
Q2: How does integrated welding mold opening customization solve the welding deformation problem?
A: Aluminum alloy welding deformation is a pain point in the industry. In the integrated model, the deformation compensation amount is planned from the cross-section design stage. The weld layout and structural rigidity of multi-piece splicing are optimized simultaneously, and a welding deformation margin is reserved in the profile cross-section design. The supporting artificial aging process releases the internal stress of extrusion, and performs positioning welding and fixation before welding, along with reasonable welding sequence and parameter control. The dimensional accuracy of the frame after welding can be controlled within ±1mm/3m.
Q3: What welding processes are supported by integrated mold opening and customization for aluminum profile welding?
A: Matching MIG/TIG argon arc welding (suitable for general aluminum alloy frames and equipment racks, with high weld quality), gas shielded welding (high efficiency, suitable for batch welding of structural parts), and friction stir welding (high weld strength, small deformation, no pores, suitable for aerospace, military and other scenarios with high requirements for welding quality). Our company recommends the most suitable welding process based on the stress conditions and quality requirements of the welded structural parts.
Q4: What materials can be used for integrated welding mold opening customization?
A: 6061-T6 (high-strength welded structure with the strongest versatility), 6063-T5 (general-purpose welded frame with good formability), 6005-T6 (fatigue-resistant welded structure suitable for high-frequency dynamic load scenarios), and 5083 (corrosion-resistant welded structure suitable for marine environments or chemical equipment) are available. The welding structure design can effectively improve the connection strength and achieve high-strength structural support compared to the standard aluminum profile assembly parts connection method.
Q5: What is the weld strength achieved by integrated welding mold opening and customization?
A: Weld strength ≥ 85% of base material. Products welded using friction stir welding technology have high weld strength, small deformation, and no pores, making them suitable for scenarios with high requirements for welding quality. Our company can cooperate with the EN 15085-2 rail vehicle welding certification system, providing welding quality inspection reports for each batch, and ensuring traceability of key welds.
Q6: What is the minimum order quantity and delivery time for integrated welding mold opening customization?
A: The minimum order quantity supports small batch customization (starting from 50kg). The conventional structural mold opening cycle is 10-15 days for sampling, and the batch delivery date is 15-20 days after the sample is confirmed. Because integrated welding mold opening involves the synergy of extrusion and welding processes, the delivery time is longer than that of pure mold opening customization. It is recommended to communicate welding requirements and structural design in advance.
GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:Aluminum profile welding integrated mold opening