
Automated logistics
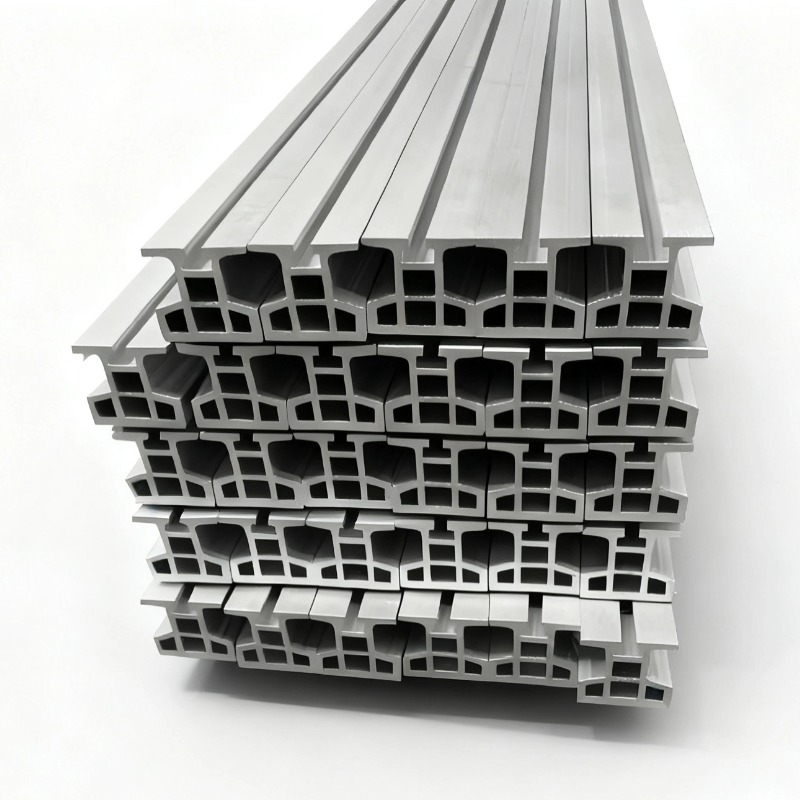
EMS Suspension Rail - Fatigue Life and Joint Detail
Six million cycles over twenty years, and the section is not what fails. Where an EMS rail actually cracks: joints, splices, weld toes and hanger bolts.
Product Details
A final assembly EMS rail is specified for takt time, and then it is expected to survive twenty years. Those two requirements point in opposite directions. A rail optimised for takt is stiff and light; a rail that survives twenty years is one whose joints and attachments have been designed for a fatigue life, not for a static load.
The main EMS rail page covers takt, joint quality and conductor integration. This page is about the number that never appears on a data sheet: how many cycles the rail will see, and which part of it will fail first.
Do the cycle count before choosing the section
A line running 60 jobs per hour, two shifts, 300 days a year, puts each trolley position through about 288,000 cycles a year. Over twenty years that is 5.8 million cycles. If a vehicle passes a given point more than once per job — a return loop, an empty-carrier pass — multiply accordingly.
Aluminium does not have a true fatigue limit. Steel has a stress below which it will survive indefinitely; aluminium does not, and its S-N curve keeps descending past ten million cycles. That means a rail for a high-cycle line cannot be designed by checking that the stress is "below the fatigue limit", because there is no such number. It has to be designed against a stated life.
The usual approach for structural aluminium in this kind of duty is to keep the nominal stress range at or below about 30 to 40 MPa at the detail that will see the most cycles, and to verify the detail itself — not the parent section — against the appropriate category.
Specifications
| Item | Reference value | Notes |
|---|---|---|
| Alloy and temper | 6063-T5 or 6061-T6 | 6061-T6 where wheel loads are concentrated |
| System load | 500–2000 kg | Vehicle plus carried body |
| Running speed | 10–100 m/min | 0.17–1.67 m/s; impact rises with speed squared |
| Bending error | Reference ≤ ±0.4 mm | On roll-bent curved sections |
| Arc accuracy | Reference ≤ 0.5° | Angular error over the curved segment |
| Integrated conductor slot | Formed in the extrusion | Fixed at die design; not retrofittable |
| Joint step | Reference ≤ 0.2 mm on the running face | The single most fatigue-critical feature |
Reference values are from shipped work. The value on your order is set by your drawing, and we confirm the achievable bending accuracy and joint step in writing before you order.
The parent section is not where fatigue starts
Run the numbers on a typical EMS rail and the bending stress in the parent section is modest. A 500 kg wheel load on a 2 m hanger span produces a bending moment of about 2.5 kN·m, which in a section with 2,000 cm⁴ of inertia gives a surface stress around 6 MPa. Against a fatigue range of 30 to 40 MPa that is comfortable.
So the section is rarely the problem. What fails is one of four things, and all of them are details:
- The joint. A step of 0.5 mm at 1.5 m/s is an impact, and the local stress at the edge of the step can be several times the nominal bending stress. The joint is also where the two rail ends are least constrained, so it moves as well as loads.
- The splice connection. Bolted splice plates in slotted holes allow micro-movement under every pass, and micro-movement in aluminium frets the surface and initiates a crack at the hole edge.
- Welded attachments. A welded bracket on an extrusion creates a heat-affected zone with reduced strength and, in 6xxx alloys, a risk of hot cracking if the filler is wrong. Weld toes are the classic fatigue initiation site.
- The hanger connection. If the hanger bolt clamps through a thin flange, the flange deflects under load and the bolt sees a reversing bending moment rather than a steady tension.
This is why we would rather machine an attachment and bolt it with a dowel than weld a bracket on. A machined and dowelled joint has a definable stress concentration; a weld toe does not.
Speed raises the impact faster than it raises the load
Going from 30 to 90 m/min triples the speed but does not triple the fatigue damage. The energy in a step impact goes with speed squared, and the number of cycles also goes up because the line runs faster. Combined, the damage rate per year can rise by an order of magnitude across that speed range.
The practical consequence is that a rail that survives at low speed with a 0.5 mm joint step may fail at high speed with the same step. If the line is specified for 100 m/min, the joint tolerance has to be tightened at the design stage rather than discovered in service, because the joints cannot be improved later without replacing sections.
Curves make it worse. In a curve, the trolley's guide rollers are loaded laterally and the rail is loaded in its weak axis. Both the stress and the number of load reversals per pass go up, which is why curves and their entry and exit transitions are where cracks are usually found first.
What a twenty-year design actually looks like
The design decisions that extend life are not expensive, but they have to be made before the first drawing is released:
- Machine the joints, do not cut them. A sawn end has a burr and a squareness error; a machined end has a controlled face that can be brought to within 0.1 mm.
- Dowel every joint. Two dowels carry shear and stop the micro-movement that frets the bolt holes.
- Put a hanger at every joint. A joint at mid-span bends under every pass; a joint over a support does not.
- Avoid welds in the running section. Where a bracket is unavoidable, bolt and dowel it. Where welding is unavoidable, use the correct 5xxx filler and post-weld treatment, and expect a reduced fatigue category at that point.
- Keep the conductor slot out of the high-stress zone. A slot in a flange removes material exactly where the bending stress is highest.
Where it does not fit
Four cases where an aluminium EMS rail is the wrong answer. If the vehicle load exceeds about two tonnes per trolley, the section needed for stiffness becomes heavy enough that a steel rail is more economical, and the aluminium weight advantage disappears. If the line runs in a paint shop oven zone above about 80 °C, the temper is affected and a steel or a different alloy family is needed. If the required life is expressed in tens of millions of cycles with high wheel loads, the fatigue case becomes controlling and a steel running strip on an aluminium body is the more reliable route. And if the layout is still changing during the build, the joint positions will move — and joint positions are exactly what the fatigue design depends on, so the design should not be frozen until the layout is.
What to send for a quote
- Jobs per hour, shifts per day, and the expected service life in years — so the cycle count can be calculated.
- Vehicle and body weight, number of wheels, and the wheel material.
- Running speed on straights and through curves.
- The layout with joint positions, or the maximum rail length that can be supplied in one piece.
With those we can tell you where the joints should sit, which is the single decision that most affects how long the rail lasts.
FAQ
What bending accuracy and joint step can you hold?
Reference ±0.4 mm bending error and 0.5° arc accuracy on roll-bent sections, with 0.2 mm joint step on the running face. On a high-cycle line the joint step matters more than the bending error, because the step is felt on every pass and the bend error is felt once per lap. The value on your order is set by your drawing, and we confirm the achievable figures in writing before you order.
How long will the rail last?
That depends on the joint quality and the attachments more than on the section. A rail with machined, dowelled joints over hangers will outlast a rail with sawn, bolted joints at mid-span by a large margin under the same load and speed. We design to a stated cycle count, so tell us the life you need.
Can brackets be welded onto the rail?
They can, but we would rather not. A weld on a 6xxx extrusion creates a heat-affected zone at roughly half the parent strength and a weld toe that initiates fatigue cracks. A machined, bolted and dowelled bracket is predictable and replaceable.
Does the rail need to be stress-relieved after bending?
For a straightness-critical run, yes. Roll bending leaves residual stress that shows up as spring-back variation between sections and as gradual movement in service. A controlled stretch or thermal treatment before machining stabilises the section.
Why does my rail crack at the curves?
Because the curve loads the section in its weak axis and the guide rollers add a lateral reversing load. Combined with a joint or a bracket at the curve, the stress concentration is at its highest exactly where the load reverses most often. Put joints and brackets away from the curve if the layout allows.
How do I check the rail in service?
Look at the joint steps and the bolt holes first, not the middle of the spans. A step that has grown, or a bolt hole that has become oval, is the earliest visible sign of the mechanism that leads to a crack.
Next step
Send the takt, the vehicle weight and the expected life. We will come back with a joint layout, a hanger arrangement and a note on which details carry the fatigue risk, so the line is designed for its service life rather than for its commissioning load.
Email: linjunbing@truetrustlv.com | Call or WhatsApp: +86 136 6644 0600
GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:EMS Suspension Rail - Fatigue Life and Joint Detail