
Automated logistics
Dense-Storage Shuttle Rail
Still wasting space on forklift aisles in dense storage racks for intelligent warehousing? Are shuttle rails rusting and wearing in the low-temperature, high-humidity environment of cold-chain warehouses? Do mother-child shuttles always run less smoothly
Product Details
Still wasting space on forklift aisles in dense storage racks for intelligent warehousing? Are shuttle rails rusting and wearing in the low-temperature, high-humidity environment of cold-chain warehouses? Do mother-child shuttles always run less smoothly when changing levels?
These problems can be solved all at once by dense-storage shuttle rails.
The mother-child shuttle system is the core technical solution for intelligent dense storage. The child shuttle runs along rails within the rack aisle, responsible for storing and retrieving palletized goods; the mother shuttle transfers laterally between aisles, responsible for dispatching child shuttles to different aisles. This system eliminates forklift aisles and greatly improves warehousing space utilization, and is especially suitable for high-density storage scenarios such as cold-chain warehousing, e-commerce distribution centers, and food and pharmaceutical industry dense storage.
The shuttle rail is the foundational load-bearing component of the mother-child shuttle system; rail accuracy directly determines shuttle running stability, positioning accuracy, and long-term system reliability.
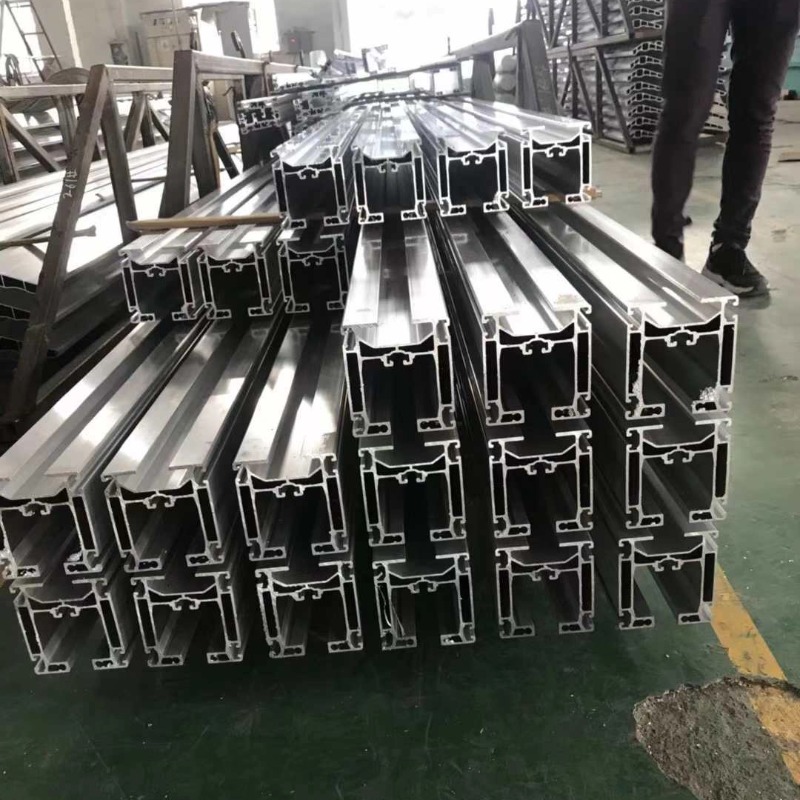
The material is 6063-T5 or 6061-T6 high-strength aluminum alloy, combining lightweight, high precision, and wear resistance. CNC one-piece finish machining, straightness ≤1.0mm/10m, dimensional tolerance±0.02mm to ±0.04mm. We can custom-make cross-sections such as in-aisle shuttle rails, mother-child shuttle level-change rails, and direction-change rails, integrating functional structures such as guide slots, mounting fixing positions, and sensor card slots, formed in one extrusion. The rail running surface can be hard-anodized for wear resistance, suiting high-frequency reciprocating handling and heavy-load conditions of shuttles. Compatible with10kg-2000kgshuttles of different specifications. Especially suited to the harsh low-temperature, high-humidity environment of cold-chain warehousing, with excellent corrosion resistance.
Core advantages at a glance:
| Advantage dimension | Technical index | Customer value |
|---|---|---|
| 📦 Wide load range | 10kg-2000kg | Covers the full range of storage needs from totes to pallets |
| 🎯 High precision | Straightness≤1.0mm/10m, tolerance ±0.02mm to ±0.04mm | Shuttles run smoothly and position accurately |
| 🛡️ Wear reinforcement | Hard anodizing (running-surface wear treatment) | Low loss from high-frequency reciprocating running, long life |
| ❄️ Cold-chain compatible | Corrosion-resistant, low-temperature resistant (-25℃) | Stable operation in low-temperature, high-humidity cold-chain environments |
| 🔧 Functional integration | Guide slot / mounting position / sensor card slot, integrally extruded | Reduces subsequent processing, easy to install |
| ⚡ Fast delivery | Samples in 7-10 days for standard specs, MOQ 50kg | Project timeline under control |
Shuttle rail vs stacker crane floor rail:
| Comparison dimension | Shuttle rail | Stacker crane floor rail |
|---|---|---|
| Installation position | Inside rack / rack bottom | Floor |
| Load-bearing object | Shuttle (child / mother vehicle) | Stacker crane |
| Cross-section design | Narrow, compact, suits shuttle guide wheels | Wide, heavy, suits stacker crane running wheels |
| Functional integration | Guide slot / sensor card slot / mounting position | Relatively simple |
| Environmental requirements | Cold-chain / room temperature / cleanroom all suitable | General industrial environment |
| Corrosion resistance requirements | High (cold-chain high-humidity environment) | General |
Dense-storage shuttle rail vs ordinary conveyor line rail:
| Comparison dimension | Shuttle rail | Ordinary conveyor line rail |
|---|---|---|
| Running mode | Shuttle self-travels | Conveyor line continuous or intermittent conveying |
| Accuracy requirements | High (straightness ≤1.0mm/10m) | General (straightness ≤1.0mm/10m) |
| Functional integration | Guide slot / sensor card slot / mounting position | Relatively simple |
| Wear requirements | High (high-frequency reciprocating running) | General |
| Applicable scenarios | Intelligent warehousing / dense storage / cold chain | General conveyor lines |
Applicable scenarios (find your match):
| Application field | Typical use | Compatible load | Key requirements |
|---|---|---|---|
| Mother-child shuttle system | In-aisle shuttle rail | 10-2000kg | High precision, wear-resistant |
| Dense-storage racks | Dense storage rack supporting rails | 100-1500kg | High space utilization |
| Cold-chain warehousing | Low-temperature cold-storage shuttle rails | 100-1000kg | Low-temperature resistant, corrosion-resistant |
| E-commerce distribution centers | High-speed sorting shuttle rails | 10-500kg | High-frequency running, precise positioning |
| Food and pharmaceutical industry | Dense storage shuttle rails | 100-1000kg | Clean surface, corrosion-resistant |
| Mother-child vehicle level change | Level-change rails, direction-change rails | 100-2000kg | Perpendicularity, splicing accuracy |
01 A00 primary aluminum ingot—the quality source of shuttle rails
Produced fromA00-grade primary aluminum ingot, containing no scrap aluminum, with uniform material and stable mechanical properties, ensuring the fatigue resistance and dimensional stability of shuttle rails under long-term high-frequency reciprocating running conditions. The dense microstructure of primary aluminum ingot is key to ensuring rails bear load long-term without deformation.
02 High-precision CNC machining—shuttles run smoothly and accurately
ThroughCNC one-piece finish machining, the rail surface is flat and burr-free, and does not easily deform.
-
Straightness accuracy≤1.0mm/10m
-
Dimensional tolerance±0.02mm to ±0.04mm
-
Ensures shuttles run smoothly within rack aisles and position accurately
03 Wear reinforcement—low loss from high-frequency reciprocating running
The rail running surface can behard-anodized for wear resistance(HV≥300), with wear resistance over 3 times that of ordinary anodizing.
-
Suits high-frequency reciprocating handling and heavy-load conditions of shuttles
-
Low long-term running loss, low maintenance cost
-
Especially suited to the harsh low-temperature, high-humidity environment of cold-chain warehousing
04 Functional structure integrated design—easy to install
The rail cross-section can integrateguide slots, mounting fixing positions, sensor card slotsand other functional structures, formed in one extrusion, reducing post-processing steps and making installation convenient.
05 Full-process one-stop delivery—deal with only one window
From mold development, extrusion to CNC finish machining and surface finishingone-stop delivery, so customers only deal with one supplier. Rail cross-section dimensions, rail length, and mounting hole positions can all be custom-made to drawings.
Complete machining capability parameters:
| Item | Parameter / Description |
|---|---|
| Applicable scenarios | Intelligent warehousing mother-child shuttle systems, dense-storage rack support |
| Alloy material | 6063-T5 / 6061-T6 |
| Rail form | In-aisle shuttle rails, mother-child vehicle level-change rails, direction-change rails |
| Straightness | ≤1.0mm/10m |
| Dimensional tolerance | ±0.02mm to ±0.04mm |
| Applicable load | 10kg-2000kg(compatible with shuttles of different specifications) |
| Surface treatment | Anodizing, hard anodizing (running-surface wear treatment) |
| Functional integration | Guide slots, mounting fixing positions, sensor card slots |
| Customization range | Rail length, cross-section dimensions, and mounting hole positions can all be customized |
| Extrusion length | Up to20M |
| Extrusion equipment | 600T-12000T (partner production lines) |
| Machining equipment | CNC machining centers |
| Executive standard | GB/T 6892-2023, ISO9001 |
| MOQ | 50kg |
| Production location | Qingpu, Shanghai |
Typical application scenarios:
-
Intelligent warehousing mother-child shuttle systems
-
Dense-storage rack rails
-
Automated stereoscopic warehouses
-
Cold-chain warehousing logistics
-
E-commerce distribution centers
-
Intelligent factory material handling
-
Dense storage in the food and pharmaceutical industry
-
Mother-child vehicle level-change rails / direction-change rails
FAQ (Frequently Asked Questions)
Q1: What is the difference between a mother-child shuttle system and a stacker crane stereoscopic warehouse?
A: The mother-child shuttle system is a dense storage solution that eliminates forklift aisles; child shuttles run within rack aisles to store and retrieve goods, and mother shuttles transfer laterally between aisles, greatly improving warehousing space utilization, and is especially suitable for cold-chain warehousing, e-commerce distribution centers, and food and pharmaceutical industry scenarios with high storage density requirements. The stacker crane stereoscopic warehouse is an automated storage and retrieval solution in which the stacker crane travels along the floor rail and uses a fork to store and retrieve goods between racks. We can provide the core rails for both solutions, with selection based on the customer's warehousing mode.
Q2: What is the difference between shuttle rails and stacker crane floor rails?
A: Shuttle rails are installed inside the rack or at the rack bottom, and shuttles run on the rails to store and retrieve goods; the rails are usually narrow with compact cross-sections, matching shuttle guide wheel dimensions. Stacker crane floor rails are installed on the floor, and the stacker crane travels along the floor rail in the aisle. The two have similar material and machining accuracy requirements (6061-T6/6063-T5, straightness ≤1.0mm/10m), but differ in cross-section design and installation method. Shuttle rails have higher corrosion resistance requirements for low-temperature, high-humidity cold-chain environments.
Q3: What is the load range of shuttle rails?
A: Compatible with10kg-2000kgshuttles of different specifications, covering diverse storage needs from light-load totes to heavy-load pallets. Light shuttles (≤300kg) can use 6063-T5 material; heavy shuttles (500kg-2000kg) require 6061-T6 material.
Q4: Why do shuttle rails require hard anodizing?
A: Shuttles run at high frequency back and forth on the rails, with wheels rubbing against the rail running surface long-term. Hard anodizing forms a high-hardness oxide layer (HV≥300) on the running surface, with wear resistance over 3 times that of ordinary anodizing, significantly extending rail service life and reducing maintenance cost. It is especially suited to low-temperature, high-humidity cold-chain environments.
Q5: What special requirements does cold-chain warehousing impose on shuttle rails?
A: The low-temperature, high-humidity environment of cold-chain warehousing imposes higher requirements on rail corrosion resistance and fatigue strength. Our rails use 6061-T6 high-strength aluminum alloy + hard anodizing, capable of long-term stable operation in-25℃low-temperature environments, with excellent corrosion resistance, effectively coping with condensation erosion and temperature changes in cold-chain warehousing.
Q6: What is the difference between child vehicle rails and mother vehicle rails?
A: Child vehicle rails are installed within rack aisles; the child shuttle runs along the rail to store and retrieve goods, and the rail cross-section is usually narrow with high straightness requirements. Mother vehicle rails are installed in the lateral aisle between rack rows; the mother shuttle moves laterally on the rail, responsible for dispatching child shuttles to different aisles, and the rail cross-section is usually larger with stronger load-bearing capacity. We can custom-make both rail types, supporting special cross-section designs such as level-change rails and direction-change rails.
Q7: Which shuttle brands is the shuttle rail compatible with?
A: It is compatible with mainstream domestic and international mother-child shuttle brands such as Huazhang, Kejie, BRI, Kunship, Swisslog, and SSI Schaefer, as well as various customized shuttle systems. The customer provides shuttle technical parameters or guide wheel drawings, and we custom-match the rail cross-section dimensions and mounting interfaces according to brand specifications.
Get a solution now
📞 Contact Manager Du:13611846009
Provide shuttle specifications or dense-storage layout drawings, and the engineering departmentwithin 2 hourswill give a rail model recommendation and solution assessment.
Free technical consultation | Shuttle rail solution design | Direct from source factory

GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:Dense-Storage Shuttle Rail