
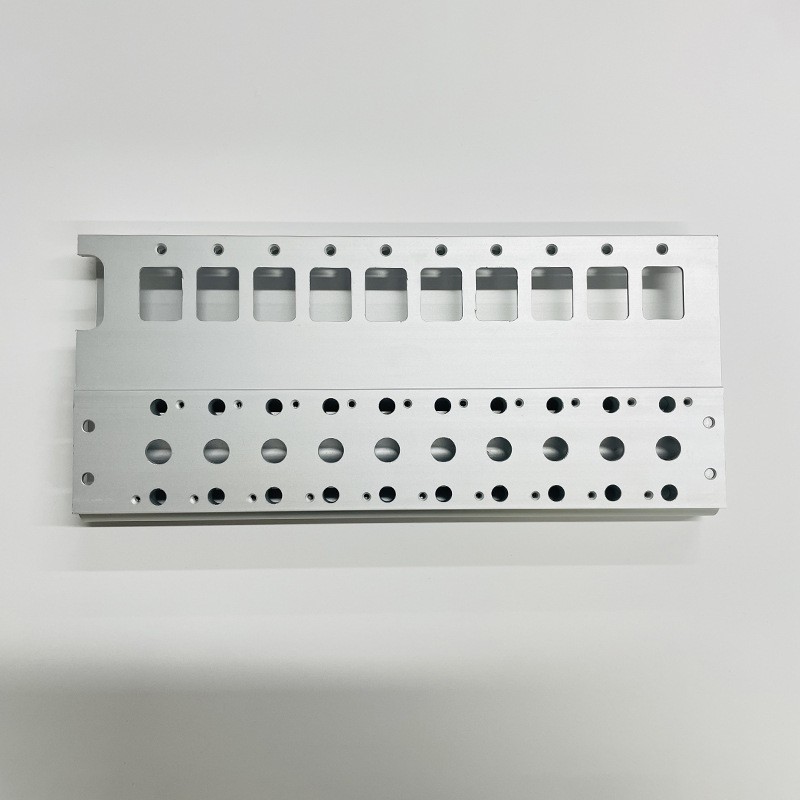
Aluminum Product Processing
Aluminum Profile CNC Drilling and Tapping
Aluminum profile CNC drilling and tapping is one of the core processes in aluminum profile deep processing; almost all aluminum profile structural parts require drilling and tapping to achieve connection and assembly. Hole machining accuracy directly dete
Product Details
Aluminum profile CNC drilling and tapping is one of the core processes in aluminum profile deep processing; almost all aluminum profile structural parts require drilling and tapping to achieve connection and assembly. Hole machining accuracy directly determines the assembly quality and overall rigidity of the frame structure - hole position deviation causes assembly jamming and structural skewing; insufficient thread accuracy causes bolt loosening or seizing.
Shanghai Chuangsi Aluminum Co., Ltd. is located in Qingpu, Shanghai, with its own physical factory equipped with CNC drilling and tapping centers and automatic tapping machines. Using high-rigidity precision spindles and rigid tapping technology, drilling and tapping are completed in one operation without a second tool change. Hole position accuracy is stably controlled at ±0.02mm, thread accuracy meets the 6H grade standard, and tapping depth accuracy is ±0.1mm. Compared with manual drilling or ordinary bench drill processing, CNC drilling and tapping offers significant advantages in high precision, good consistency and high efficiency, especially suitable for the hole machining needs of batch parts.
Targeting the thin-wall and easy-to-deform characteristics of aluminum profiles, we use dedicated fixtures to optimize the clamping scheme and effectively control machining deformation. One-stop delivery from profile cutting, drilling and tapping to surface treatment - customers only need to provide drawings, and we handle the entire process.
Core machining capabilities:
1. Precision drilling: Equipped with CNC drilling and tapping centers, capable of processing through holes, countersunk holes, blind holes, mounting holes and other types. Hole position accuracy ±0.02mm, hole diameter accuracy ±0.02mm, max. drilling diameter phi50mm.
2. Precision tapping: Using rigid tapping technology with synchronized spindle and feed axis control, high tapping accuracy and good thread surface quality. Thread accuracy meets the 6H grade standard, tapping depth accuracy ±0.1mm, max. tapping diameter M20.
3. Countersunk hole machining: Compatible with various countersunk screw standards (GB/T, ISO, ANSI); countersunk hole diameter and depth are precisely controlled, with countersink depth accuracy ±0.05mm, meeting assembly and fastening requirements.
4. End-face tapping and drill-tap machining: End-face tapping, side-face tapping, inclined-face tapping and other multi-angle tapping of profiles are all available, meeting the connection and assembly needs of various profiles.
5. Batch hole machining: Using multi-station fixtures + CNC program optimization, batch machining delivers good hole position consistency and low per-piece cost, suitable for high-volume standard-part hole machining.
Machining capability parameters:
| Item | Parameter / Description |
|---|---|
| Equipment Type | CNC drilling and tapping centers, automatic tapping machines |
| Hole Position Accuracy | ±0.02mm |
| Hole Diameter Accuracy | ±0.02mm |
| Tapping Accuracy | 6H grade |
| Tapping Depth Accuracy | ±0.1mm |
| Max. Drilling Diameter | φ50mm |
| Max. Tapping Diameter | M20 |
| Countersink Depth Accuracy | ±0.05mm |
| Max. Machining Length | 6500mm |
| Machining Method | Custom from drawings, custom from samples |
| Hole Type | Through holes, countersunk holes, blind holes, mounting holes, tapped holes |
| Tapping Type | End-face tapping, side-face tapping, drill-tap machining |
| Executive Standard | GB/T 6892-2023 high precision grade |
| MOQ | 50kg |
| Sample Lead Time | 3-7 days (depending on complexity) |
| Bulk Lead Time | 7-15 days after sample approval |
| Production Location | Qingpu, Shanghai |
Selection guide:
| Application Scenario | Key Machining Requirements | Common Hole Types |
|---|---|---|
| Automation equipment frame connection | High hole position accuracy, convenient installation | Through holes, countersunk holes |
| AI server heat sink mounting | Flatness ≤0.02mm, precise hole positions | Mounting holes, countersunk holes |
| Robot base fixation | Hole position accuracy ±0.02mm, high strength requirements | Through holes, tapped holes |
| Semiconductor equipment chamber | High-precision hole positions, burr-free | Blind holes, tapped holes |
| 5G communication equipment housing | Thin-wall drilling without deformation | Through holes, tapped holes |
| New energy battery module | Good hole position consistency, high batch efficiency | Through holes, countersunk holes |
Typical application scenarios:
-
Automation equipment mounting hole machining
-
Equipment frame connector drilling and tapping
-
AI server heat sink mounting holes
-
Panel and cover countersunk holes
-
Robot base fixing holes
-
Semiconductor equipment chamber mounting holes
-
5G communication equipment housing tapped holes
-
New energy battery module connection holes
FAQ (Frequently Asked Questions)
Q1: What hole types are generally included in aluminum profile drilling and tapping?
A: Mainly includes through holes (penetrating the entire profile), countersunk holes (for countersunk screw installation), blind holes (not penetrating the profile), mounting holes (equipment fixation), and tapped holes (for bolt connection after tapping). Which hole types to machine is determined according to customer assembly requirements.
Q2: What precision can aluminum profile drilling and tapping achieve?
A: Hole position accuracy ±0.02mm, hole diameter accuracy ±0.02mm, tapping accuracy 6H grade, tapping depth accuracy ±0.1mm. When the aluminum profile wall is thin, dedicated fixtures are used to control deformation, and accuracy is stably guaranteed.
Q3: What is the maximum hole diameter and thread that can be machined?
A: Max. drilling diameter phi50mm, max. tapping diameter M20. If larger holes or threads are needed, they can be completed in combination with CNC milling.
Q4: Is thin-wall aluminum profile drilling prone to deformation? How to solve it?
A: Drilling at thin-wall sections of aluminum profiles is indeed prone to deformation. We optimize the clamping scheme with dedicated fixtures and select suitable tools and cutting parameters to effectively control machining deformation. Aluminum profiles with wall thickness ≥1.5mm can all be stably machined.
Q5: What precision can countersunk holes achieve?
A: Countersink depth accuracy ±0.05mm, countersink diameter accuracy ±0.05mm, compatible with various countersunk screw standards (GB/T, ISO, ANSI), meeting assembly and fastening requirements.
Q6: Is deburring still required after tapping?
A: We provide matched deburring after tapping to ensure hole openings and thread surfaces are smooth and burr-free, meeting assembly and use requirements. If additional high-gloss treatment is needed, it can be completed during the surface treatment process.


GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:Aluminum Profile CNC Drilling and Tapping