
Aluminum Product Processing
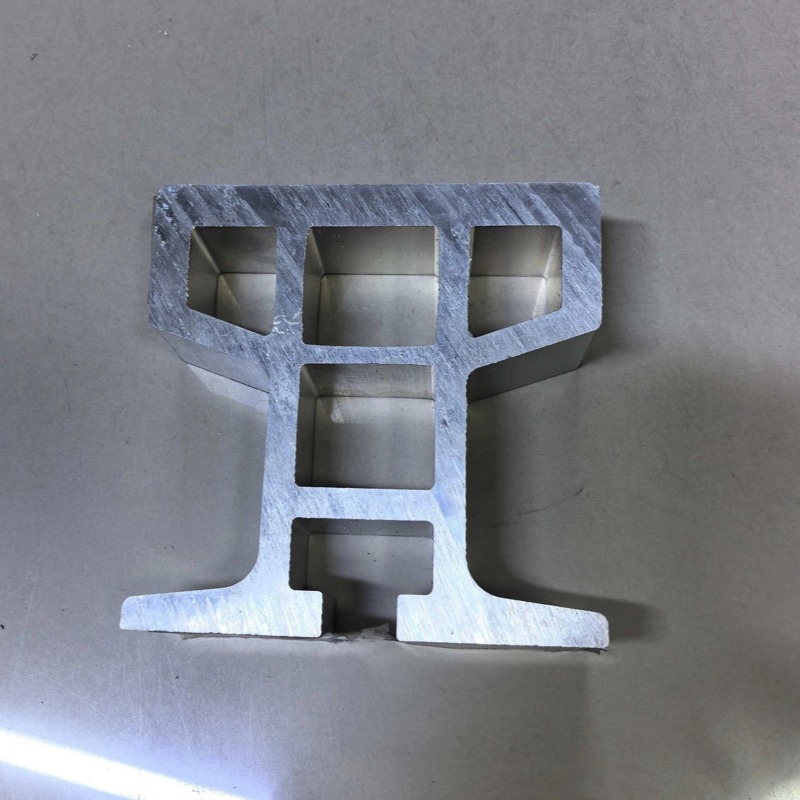
Custom Mold Development for RGV/AGV Track Aluminum Profiles
RGV (rail-guided vehicle) and AGV (automated guided vehicle) are the core handling equipment in intelligent warehousing and automated logistics systems. RGV trolleys run around the stereoscopic warehouse and interface with conveyor lines and stacker crane
Product Details
RGV (rail-guided vehicle) and AGV (automated guided vehicle) are the core handling equipment in intelligent warehousing and automated logistics systems. RGV trolleys run around the stereoscopic warehouse and interface with conveyor lines and stacker cranes to transport goods; AGVs achieve flexible path travel via magnetic strip, QR code, or laser navigation. The track is the road for these equipment — track precision directly determines whether the trolleys run smoothly, position accurately, and achieve long service life.
Aluminum alloy tracks offer clear advantages over traditional steel tracks: 40%-60% lighter weight, over 30% energy savings, 30%-50% shorter installation time, and no rust-removal maintenance required. In leading intelligent warehousing projects such as JD Asia No.1, SF Express intelligent warehouses, and J&T transfer centers, aluminum profile tracks have become the standard for RGV shuttles and EMS overhead conveyor lines.
Shanghai Chuangsi Aluminum Co., Ltd. serves the intelligent warehousing, automated logistics, and intelligent handling sectors, providing a full-process one-stop service from cross-section structural design, mold development, and profile extrusion (partner production lines) to CNC precision machining and hard anodizing.
01 Quality Starts From Raw Materials
Produced using A00 primary aluminum ingot, containing no scrap aluminum, with uniform material properties and stable mechanical performance. Material options include 6063-T5 (light-duty, ≤300kg), 6061-T6 (medium-duty, 500kg class), 6005A-T6 (heavy-duty, 1000kg class), and 7075-T6 (extra-heavy-duty), selected according to track load conditions.
02 Large-Tonnage Extrusion and Dedicated Mold Design
For the wide, thick-wall, and complex internal ribbed cross-sections required by RGV tracks, large-tonnage extruders form the profile in a single press, ensuring internal lattice density and overall structural stability. Each track cross-section has an independently designed dedicated mold that can integrate guide grooves, mounting positions, and sensor card slots. Ultra-large profiles with an circumscribed circle diameter of 600-700mm can be produced.
03 High-Precision CNC Machining
Equipped with five-axis CNC machining centers and other precision equipment, the tracks undergo integrated CNC finishing to ensure uniform overall precision and minimal joint gaps between individual profiles. Machining precision is ±0.01-0.005mm, with dimensional tolerance stably controlled within ±0.02mm to ±0.04mm. Straightness is ≤1.0mm/10m for light-duty tracks, ≤1.2mm/10m for medium-duty, and ≤1.5mm/10m for heavy-duty. Arc accuracy for circular tracks is ≤0.5°, and repeat positioning accuracy can reach ±3mm.
04 Hard Anodizing Wear-Resistant Treatment
The track running surface can be hard-anodized to achieve a surface hardness of HV≥90 and a friction coefficient as low as 0.12, effectively reducing operating noise and energy consumption. It is suitable for 2.5m/s high-speed operation and high-frequency reciprocating handling conditions, with low long-term wear and low maintenance costs.
05 Full-Process One-Stop Delivery
One-stop delivery from mold development and extrusion to CNC precision machining and hard anodizing — customers deal with only one supplier. Custom cross-section dimensions, track lengths, and curved rail radii are available per drawings, reducing on-site machining. Each batch is supplied with dimensional inspection and material inspection reports.
Machining capability parameters:
| Item | Parameter / Description |
|---|---|
| Applicable load capacity | ≤200kg (light-duty) / 500kg (medium-duty) / 1000kg and above (heavy-duty) |
| Optional material | 6063-T5 / 6061-T6 / 6005A-T6 / 7075-T6 |
| Maximum circumscribed circle | 600-700mm |
| Dimensional tolerance | ±0.02mm to ±0.04mm |
| Straightness (light-duty) | ≤1.0mm/10m |
| Straightness (medium-duty) | ≤1.2mm/10m |
| Straightness (heavy-duty) | ≤1.5mm/10m |
| Arc accuracy (circular) | ≤0.5° |
| Repeat positioning accuracy | ≤±3mm |
| Applicable running speed | ≤2.5m/s |
| Surface treatment | Anodizing, hard anodizing |
| Surface hardness | HV≥90 (hard anodizing) |
| Friction coefficient | ≤0.12 |
| Extrusion equipment | 600T-12000T (partner production lines) |
| Execution standard | GB/T 6892-2023 high-precision grade |
| Mold development lead time | 7-10 days for samples of conventional structures |
| Batch delivery lead time | 10-15 days after sample confirmation |
| Minimum order quantity | Supports 50kg-scale R&D prototyping |
| Production location | Qingpu, Shanghai |
RGV/AGV track aluminum profile selection guide:
| Track type | Recommended material | Key requirements |
|---|---|---|
| Light-duty RGV track (≤300kg) | 6063-T5 | Straightness ≤1.0mm/10m, anodizing |
| Medium-duty RGV track (500kg class) | 6061-T6 | Straightness ≤1.2mm/10m, hard anodizing |
| Heavy-duty RGV track (1000kg class) | 6005A-T6 / 7075-T6 | Straightness ≤1.5mm/10m, ultra-hard anodizing |
| AGV running guide rail | 6063-T5 | Integrated magnetic strip / QR code navigation groove |
| Curved / circular track | 6063-T5 / 6061-T6 | Arc accuracy ≤0.5°, CNC roll bending |
Typical application scenarios:
-
Intelligent warehousing RGV shuttle track systems
-
AGV automated guided vehicle running guide rails
-
Stereoscopic warehouse stacker floor rails
-
Automated conveyor line tracks
-
Circular / curved rail conveyor systems
-
EMS overhead suspended conveyor tracks
-
Express sorting center circular tracks
-
Cold chain warehousing logistics tracks
-
Heavy-duty stereoscopic warehouse load-bearing floor rails
-
Flexible manufacturing system AGV navigation tracks
FAQ (Frequently Asked Questions)
Q1: What are the advantages of RGV/AGV track aluminum profiles over traditional steel tracks?
A: Aluminum alloy tracks offer clear advantages over traditional steel tracks: 40%-60% lighter weight, over 30% energy savings, 30%-50% shorter installation time, and no rust-removal maintenance required. In leading intelligent warehousing projects such as JD Asia No.1, SF Express intelligent warehouses, and J&T transfer centers, aluminum profile tracks have become the standard for RGV shuttles and EMS overhead conveyor lines.
Q2: What straightness can RGV/AGV track aluminum profiles achieve?
A: Straightness is ≤1.0mm/10m for light-duty tracks, ≤1.2mm/10m for medium-duty, and ≤1.5mm/10m for heavy-duty. Arc accuracy for circular tracks is ≤0.5°. The tracks undergo integrated five-axis CNC finishing with minimal joint gaps between individual profiles, and repeat positioning accuracy can reach ±3mm.
Q3: Which materials are available for RGV/AGV track aluminum profiles?
A: Material options include 6063-T5 (light-duty, ≤300kg), 6061-T6 (medium-duty, 500kg class), 6005A-T6 (heavy-duty, 1000kg class), and 7075-T6 (extra-heavy-duty), selected according to track load conditions. Produced using A00 primary aluminum ingot, containing no scrap aluminum, with uniform material properties and stable mechanical performance.
Q4: What dimensional precision can RGV/AGV track aluminum profiles achieve?
A: Dimensional tolerance is stably controlled within ±0.02mm to ±0.04mm, with machining precision of ±0.01-0.005mm. Large-tonnage extruders form the profile in a single press, ensuring internal lattice density and overall structural stability.
Q5: What surface treatment options are available for RGV/AGV track aluminum profiles?
A: The track running surface can be hard-anodized to achieve a surface hardness of HV≥90 and a friction coefficient as low as 0.12, suitable for 2.5m/s high-speed operation and high-frequency reciprocating handling. Anodizing is also available to meet conventional operating requirements.
Q6: What is the minimum order quantity and lead time for RGV/AGV track aluminum profiles?
A: The minimum order quantity supports 50kg-scale R&D prototyping. Mold development for conventional structures takes 7-10 days for samples, and batch delivery is 10-15 days after sample confirmation. Custom cross-section dimensions, track lengths, and curved rail radii are available per drawings.

GET A QUOTE
Once you have submitted your requirements, we will contact you as soon as possible regarding your product inquiry.:Custom Mold Development for RGV/AGV Track Aluminum Profiles